Introduction
Why do baking cups jam on automated lines? Usually the cause is not the machine. It is a mismatch between the cup construction and the denesting mechanism: wall rigidity too low to resist the separating force, pleat geometry that lets cups interlock, surface friction that varies with humidity, or a stack compressed in transit. Each of these is a paper specification issue before it is an equipment issue. Cup programmes usually ship alongside pan lining; our private-label parchment paper supplier specs cover the sheets and rolls that pair with them.
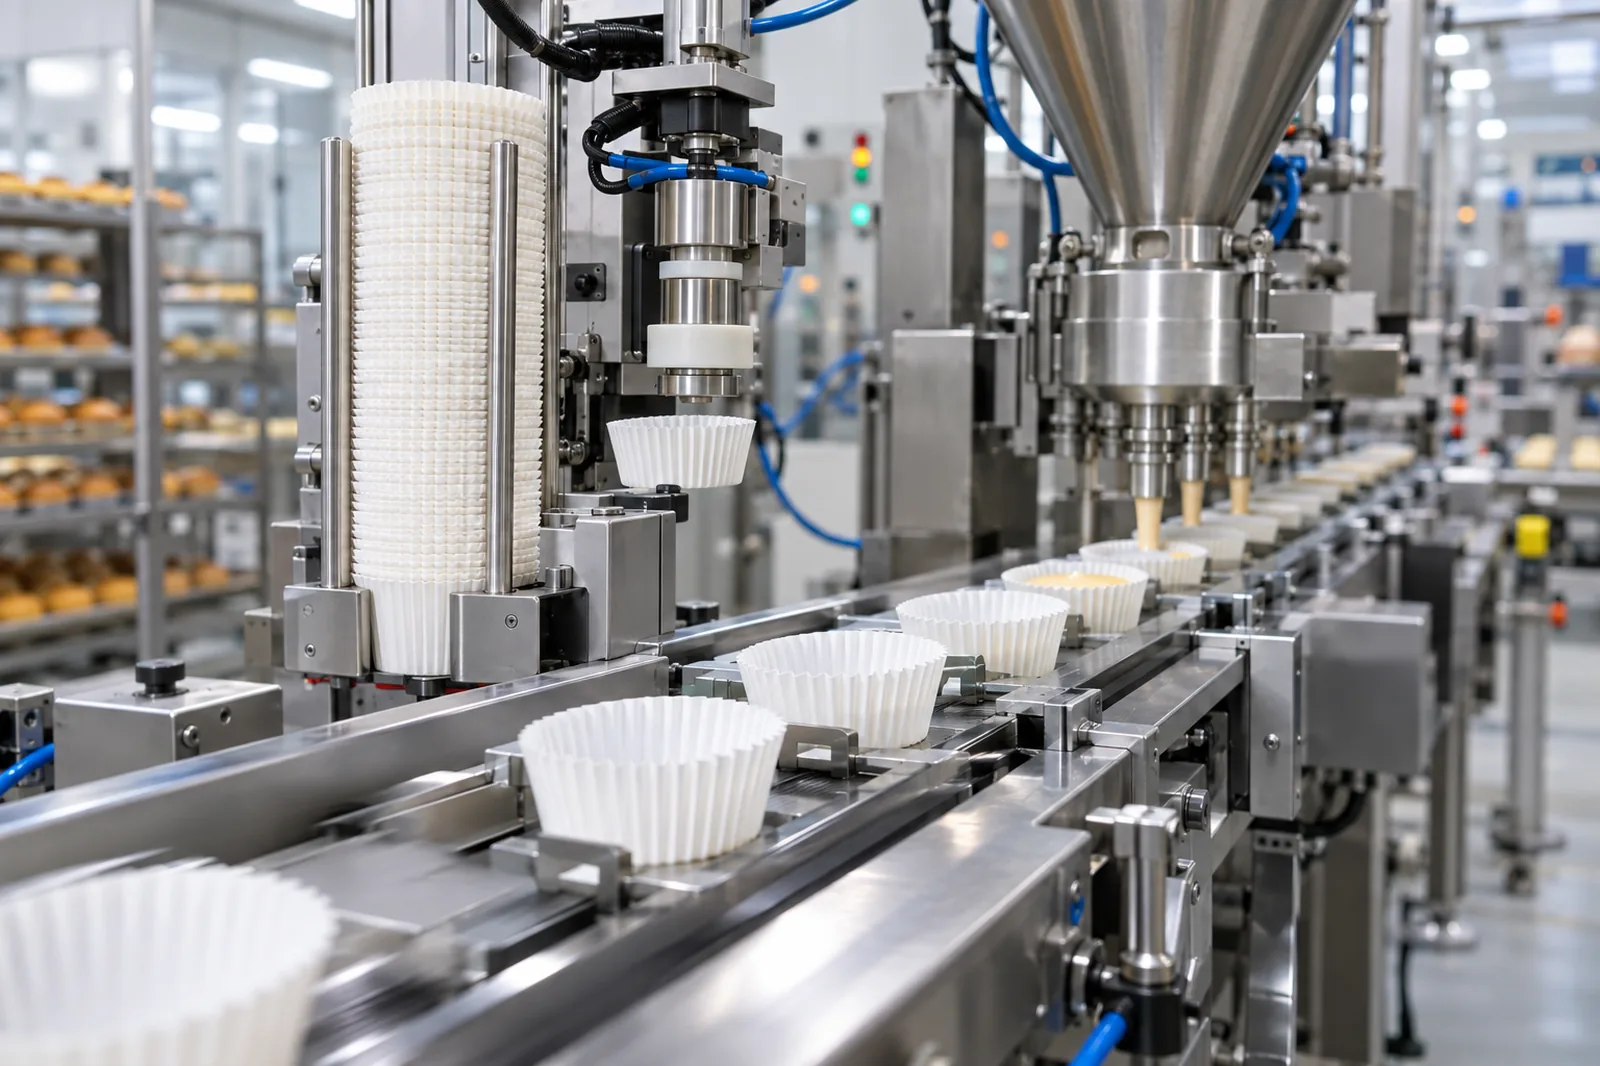
Denesting is the step where a nested stack is separated one cup at a time and placed into a tray or mould. On a hand-filled bench an operator compensates instinctively for a sticky stack. On a line running forty to eighty cycles per minute there is no such compensation: a mis-feed means double cups, dropped cups, skewed placement or a stoppage. Buyers verifying these specifications can review the certificate library alongside supplier documentation requests.
This guide is for industrial bakeries, co-packers, private-label producers and equipment buyers: what denesting performance means, how construction drives it, common jam causes, the metrics worth specifying, and how to verify a supplier.
1. What Denesting Performance Really Means
Denesting is a set of related behaviours, not one property, so specifying only "good separation" leaves suppliers guessing. Where a bakery lines trays and moulds product in the same run, our pre-cut parchment paper sheets and rounds are quoted with the cup programme for a single documentation package.
Single-cup separation is the core requirement: exactly one cup per cycle. Double feeds are the most common defect and the most visible, because a doubled cup is obviously wrong at the tray. The factory and certificate library lists the third-party audits and test reports behind these claims.
Consistent orientation means the cup leaves the stack upright and square. Cups that leave tilted, rotated or inverted jam downstream or place badly in the mould.
Repeatability across the stack matters more than the first few cups. A stack that separates cleanly at the top but binds halfway down still stops the line, so evaluate the full stack rather than a sample handful.
Rate capability means the construction holds separation at the line's real cycle speed: a cup that denests reliably at thirty cycles per minute can fail at seventy. Placement accuracy covers where the cup lands: centred, seated to depth, and stable enough to receive batter.
2. How Construction Drives Separation
Four variables determine whether a cup denests cleanly, and they interact.
Grammage sets wall rigidity. Too light and the cup collapses or folds as it is pushed into the mould; too heavy and it resists the mechanism, raising the force needed. The right value sits in a band defined by cup diameter and wall height.
Wall and pleat geometry controls how deeply cups nest. Deep nesting raises stack density and lowers freight cost, but increases contact area and interference, which raises separation force. Suppliers tune pleat count, pleat depth and the base-to-wall angle.
Friction between cups is governed by surface finish and any coating. Silicone or greaseproof treatment lowers friction and improves release from the stack, though treatment that is too heavy can make cups slide unpredictably. Embossing adds texture that either aids grip or increases interference.
Dimensional consistency is the quiet variable. Small variation in base diameter, wall height or rim curl creates irregular gaps in the stack, and irregular stacks feed irregularly. Tight tolerances cost more to hold but are the most reliable predictor of smooth automation.
3. Why Cups Jam: Practical Root Causes
Work through likely causes in order rather than adjusting the machine first.
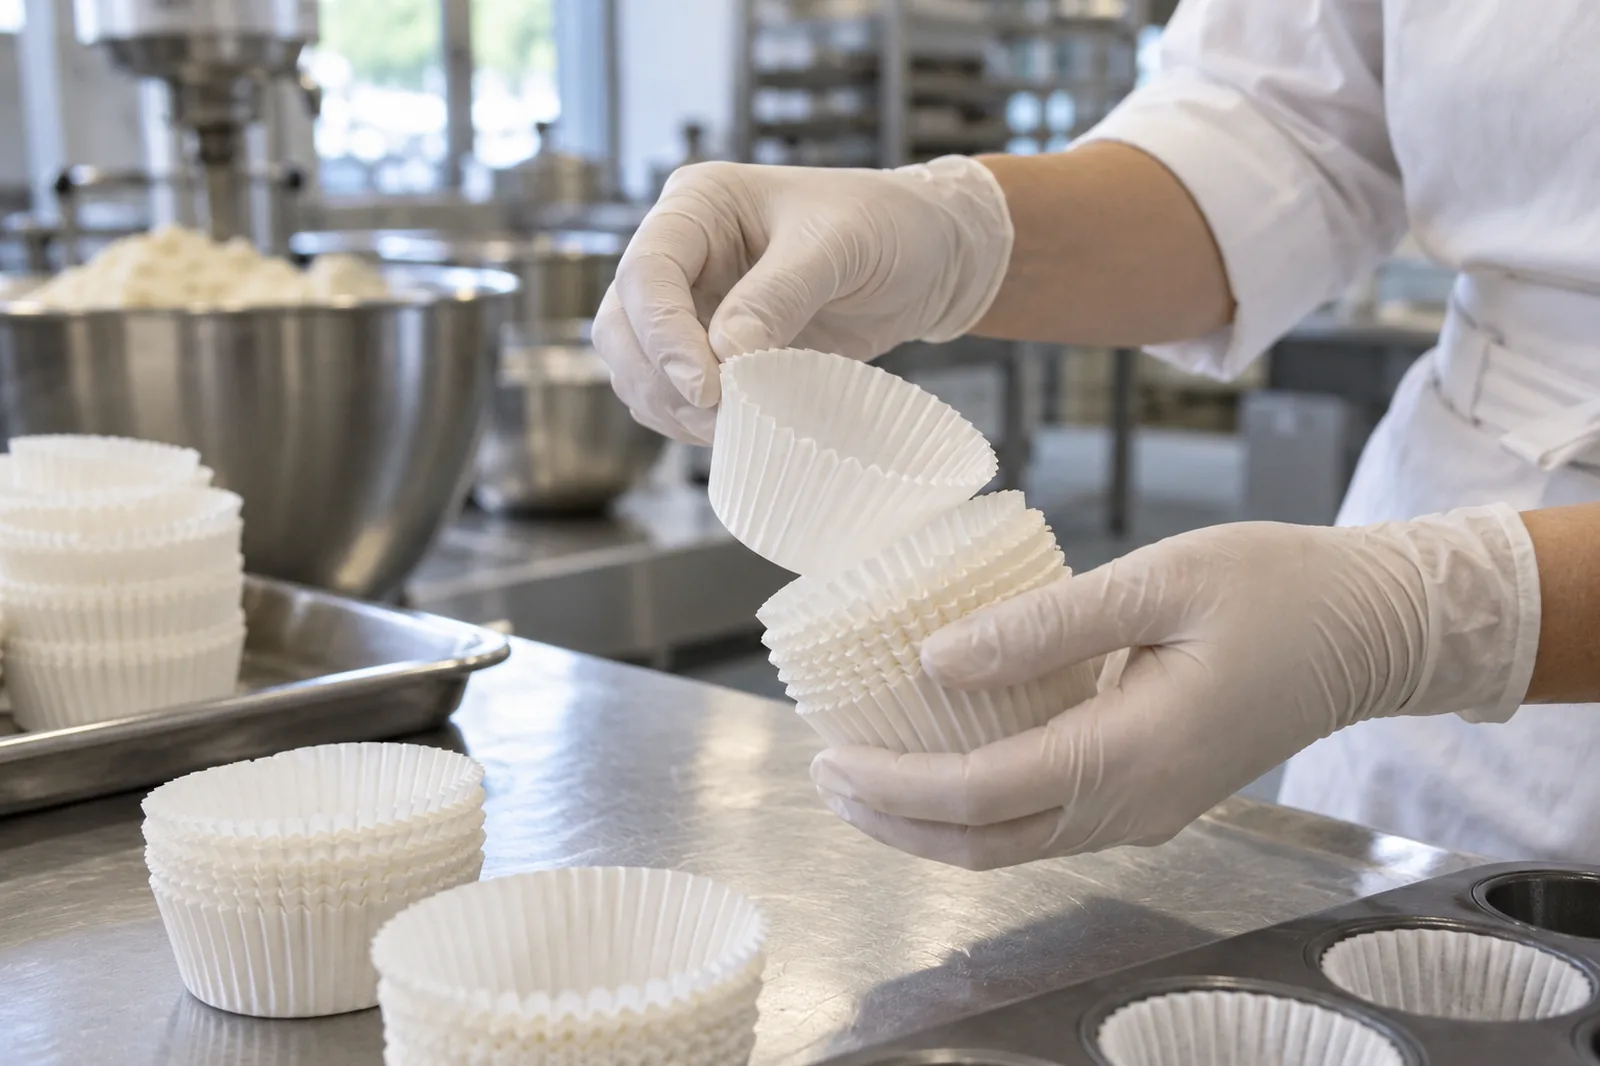
Compressed stacks are common after long transit or heavy pallet stacking: compression flattens pleats and increases contact area. Limit stack height per bundle, specify cartons with adequate crush resistance, and loosen stacks before loading.
Humidity is the most frequent environmental cause. Paper absorbs moisture, softens and becomes tackier, raising separation force and deforming cups. Store dry and temperature-stable, keep cartons sealed until use, and let product acclimatise to the production area before opening.
Static makes cups cling, especially with lightweight grades in dry conditions at high speed. Anti-static measures, humidity control and appropriate surface treatment help.
Out-of-tolerance dimensions show up as intermittent rather than constant faults, which makes them hard to diagnose. Measure base diameter, wall height and rim condition across a sample from the suspect lot.
Print and decoration can interfere: heavy ink coverage near the rim, foil effects or embossing can change friction or dimensions enough to affect feeding, so qualify the printed SKU on the line. Worn blades, wrong magazine pressure or stack height and mis-set timing look the same, so confirm with a known-good lot.
4. Metrics Worth Putting in the Specification
A denesting specification should be measurable, so acceptance is a test rather than an opinion.
State separation force: the force required to remove a single cup from a nested stack, measured with a defined fixture at a defined pull speed, with both upper and lower limits. Too high and the mechanism slips or deforms the cup; too low and cups drop uncontrolled.
State dimensional tolerances for base diameter, rim diameter, wall height and stack height for a fixed cup count — stack height tolerance is especially useful because it captures nesting-depth variation in one number.
State grammage with tolerance, plus treatment type and coat weight where coating is applied. State a double-feed rate limit as defects per thousand cycles at your cycle speed, and dimensional consistency as a range across a sample rather than an average, since averages hide the outliers that cause jams.
Finally state pack and pallet configuration, maximum stack height per bundle and carton crush resistance, because compression in transit is a specification issue rather than a freight accident.
5. Trial Design and Supplier Verification
Approval should happen on the line, not in a meeting room.
Run trials at production speed, since separation behaviour changes with cycle rate and a cup validated slowly will not necessarily run fast. Run multiple full stacks through the actual magazine and evaluate the beginning, middle and end of each, because the last third is where compressed stacks bind.
Test across lots: request samples from at least two production lots so lot-to-lot variation is visible before commitment. Test under real ambient conditions, including a summer humidity condition if your site sees one.
Record objective outcomes — double feeds per thousand, dropped cups, misplaced cups, stoppages and operator interventions — and compare candidates on the same numbers.
Request a declaration of compliance for the exact SKU, plus construction disclosure, lot traceability coding and written change control covering base paper, grammage, treatment and tooling. Tooling changes are easy to overlook and can shift pleat geometry enough to affect feeding.
6. Storage, Handling and Line Discipline
Even a well-specified cup feeds poorly if handled badly.
Store dry and temperature-stable, away from sunlight and external walls where condensation forms, off the floor and sealed until use. Rotate stock by lot, stay within the specified pallet height, and loosen compressed stacks before loading the magazine correctly.
Train operators to log faults by type and lot. Distinguishing double feeds from drops from misplacement turns a vague complaint into a diagnosis and gives the supplier the data to fix the right variable. Keep the mechanism maintained: separating components wear, and worn parts produce faults identical to a paper defect.
Conclusion
Automated denesting is a paper specification outcome before it is an equipment outcome. Specify the four variables that matter — grammage for rigidity, pleat geometry for nesting depth, surface treatment for friction, dimensional tolerance for consistency — then measure what you care about: separation force with limits, dimensional ranges rather than averages, and a double-feed rate at your real cycle speed. Approve across multiple lots on your own line, add storage discipline and a fault log, and most jams become diagnosable. Buyers standardising on one paper supplier can review our custom printed baking parchment paper next to their cup specifications.
What does denesting mean for baking cups?
Denesting is separating a nested stack into individual cups for placement into a tray or mould. The mechanism must take exactly one cup per cycle, upright and accurately placed, at production speed.
What causes baking cups to jam on automated lines?
The usual causes are compressed stacks from transit, humidity softening the paper, static cling, out-of-tolerance dimensions, and print or embossing that changes surface friction.
How is separation force measured?
It is the force needed to remove one cup from a nested stack, measured with a defined fixture at a defined pull speed. Agree the method with the supplier and set both upper and lower limits.
Does higher grammage improve denesting?
Not always. Heavier paper adds rigidity but also resists the mechanism. The right grammage depends on cup diameter, wall height and the feed mechanism, so validate it on your line.
Should printed cups be qualified separately from plain cups?
Yes. Ink coverage, foil and embossing can change surface friction and dimensions enough to alter feeding, so qualify the printed SKU on the line at production speed.
How should baking cups be stored to protect denesting?
Store dry and temperature-stable, sealed until use, off the floor, within the specified pallet height and rotated by lot. Let cartons acclimatise before opening.
CTA
Send LANGMAI your cup dimensions, grammage requirements, decoration route, line speed and denesting mechanism type, plus volumes and destination market. The team can propose constructions matched to automated feeding, arrange multi-lot samples for on-line trials and prepare a measurable specification with separation-force and tolerance limits.